Main Menu
Colorant Masterbatch is more than concentrated pigment in plastic pellets. It is a controlled formulation containing pigments, additives, and a compatible carrier resin. During extrusion or injection molding, processors add these pellets to natural polymer. The mixture then creates consistent color across bottles, films, pipes, toys, and automotive components.
The scale is significant. PlasticsEurope’s Plastics—The Fast Facts 2024 reports 413.8 million tonnes of global plastics production in 2023. That volume makes color consistency a manufacturing issue, not merely a design preference. Smithers’ The Future of Masterbatch to 2028 also evaluates demand by polymer, application, and region. Its analysis highlights the continuing importance of efficient dosing, dispersion, and material performance. Dr. Wolfgang Huber, a long-standing masterbatch specialist at Gabriel-Chemie, states, “Color is only successful when it remains stable throughout processing.” That principle matters on a factory floor. A poorly dispersed blue pellet can leave streaks, weak spots, or uneven surfaces. Operators may notice the defect only after thousands of parts are molded.
This guide explains how Colorant Masterbatch works, how manufacturers select carrier systems, and why dosage affects shade accuracy. It also considers lightfastness, heat stability, recyclability, and polymer compatibility. Market estimates do not always agree. Definitions and regional coverage vary. That limitation deserves attention. Still, production data and processor experience point in the same direction: reliable color requires formulation science, process control, and testing—not visual judgment alone.
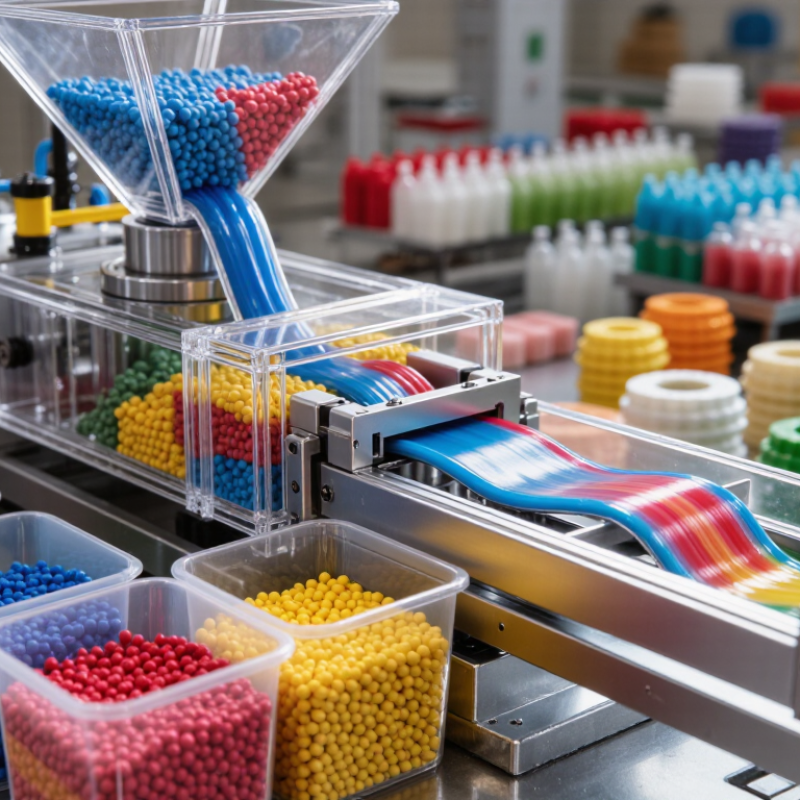
Colorant masterbatch is a concentrated mixture of pigments or dyes and a carrier resin. It usually appears as small, uniform pellets. Manufacturers add these pellets to natural polymer during processing. Heat then disperses the color through the melt.
The carrier should match, or closely suit, the base plastic. A polyethylene carrier often works with polyethylene film, while engineering plastics may need another system. Pigment selection affects shade, opacity, weather resistance, and processing stability. A technician may measure the let-down ratio, such as one part masterbatch to twenty parts resin. The exact ratio depends on the desired color and pigment strength. This calculation matters on an actual production floor.
Colorant masterbatch is used in injection molding, extrusion, blow molding, and some fiber applications. Operators mix it with pellets before feeding the hopper. Good dispersion prevents streaks, specks, and uneven surfaces. Dry storage also helps, especially when moisture-sensitive materials are involved. In my experience, a color that looks correct in a sample plaque can shift inside a thicker product. Lighting, wall thickness, and cooling conditions can change its appearance. It is not a universal solution. Small production trials remain necessary, even when the formulation seems reliable. A batch may still need adjustment.
| Data Dimension | Typical Information | Practical Significance |
|---|---|---|
| Definition | A concentrated mixture of pigments or dyes dispersed in a polymer carrier and formed into pellets. | It provides a controlled and convenient way to add color during plastic processing. |
| Main Components | Colorant, carrier resin, dispersing or processing additives, and, where required, stabilizers. | The carrier and additives influence dispersion, compatibility, surface appearance, and processing behavior. |
| Common Colorants | Organic pigments, inorganic pigments, carbon black, titanium dioxide, and selected soluble dyes. | The choice depends on the required shade, opacity, weatherability, heat resistance, and regulatory conditions. |
| Typical Colorant Loading | Often approximately 10%–70% by mass, depending on pigment type, shade strength, and masterbatch design. | Higher loading can reduce the amount of masterbatch required, but it must still provide uniform dispersion. |
| Typical Addition Rate | Commonly about 1%–5% of the total polymer mix; exact dosage is determined by the target color and opacity. | The recommended let-down ratio should be confirmed through laboratory or production trials. |
| Carrier Compatibility | The carrier should be compatible with the base polymer, such as polyethylene, polypropylene, polystyrene, ABS, PET, or polyamide. | Poor compatibility may cause streaks, specks, uneven color, weak mechanical performance, or processing instability. |
| Processing Methods | Injection molding, extrusion, blow molding, film production, rotational molding, and fiber spinning. | The masterbatch must be selected for the temperature, residence time, shear level, and equipment used. |
| Mixing Procedure | Meter the masterbatch into the base resin, blend uniformly, and feed the mixture into the processing machine. | Accurate dosing and consistent mixing help prevent shade variation between production batches. |
| Key Performance Properties | Color strength, dispersion, opacity, heat resistance, lightfastness, weather resistance, migration resistance, and moisture level. | These properties determine whether the colored plastic remains uniform and stable during processing and service. |
| Advantages | Cleaner handling than loose pigments, accurate dosing, reduced dust, improved repeatability, and easier color changeover. | These benefits can improve production efficiency and help maintain consistent product appearance. |
| Potential Limitations | Additional material cost, possible carrier incompatibility, dosing errors, and the need for drying with moisture-sensitive polymers. | Material selection, storage, and process control are essential for reliable results. |
| Quality Checks | Color difference, moisture content, melt flow behavior, pigment dispersion, heat stability, and pellet uniformity. | Routine testing supports stable color matching and reduces defects such as streaks, spots, and color drift. |
| Typical Applications | Packaging films, containers, household products, automotive components, electrical parts, pipes, sheets, fibers, and consumer goods. | The appropriate formulation depends on the end-use requirements, polymer type, processing method, and regulatory environment. |
Colorant masterbatch is a concentrated mixture of pigment, carrier resin, and processing additives. It is not simply colored plastic. The carrier usually matches the target polymer, such as polyethylene, polypropylene, polystyrene, or engineering resin. This compatibility helps the color disperse evenly during extrusion or injection molding.
Pigments provide shade and opacity. Organic pigments can create bright colors, while inorganic pigments often offer stronger heat and weather resistance. Dispersing agents help separate pigment particles and reduce specks. Waxes or processing aids may improve feeding and mixing. Some formulations also contain stabilizers, fillers, or optical modifiers. The exact balance depends on temperature, product thickness, and outdoor exposure.
Scale matters. Plastics Europe reported global plastics production of 413.8 million tonnes in 2023. That volume creates constant demand for controlled, repeatable coloration. Professional testing still remains essential. Technicians check melt flow, color difference, migration, and heat stability against the final polymer. A masterbatch can look correct in a laboratory plaque but shift in a thin film. That assumption can fail. In practice, the first trial is rarely perfect. Excess pigment may reduce toughness, while poor dispersion can produce streaks and visible dots. ISO-based color and weathering tests provide useful control, but they cannot replace production experience. Formulators should also review technical data sheets and safety documentation before approving a recipe.
Colorant masterbatch is a concentrated blend of pigments or dyes dispersed in a carrier resin. This representative formulation shows how the main components can contribute to the overall blend: the carrier resin supports compatibility and processing, pigments provide color and opacity, dispersants improve pigment distribution, and processing additives help the material flow and perform consistently. Actual formulations vary according to the polymer, processing method, color strength, and end-use requirements.
Colorant masterbatch is a concentrated mixture of pigments or dyes, carrier resin, and additives. Manufacturers blend it into plastic during processing to create consistent color. Its production starts with selecting a colorant compatible with the target polymer. Pigment choice affects shade, opacity, heat stability, and weather resistance. The ingredients are weighed carefully, although minor variations can still influence the final color.
The materials are premixed, then fed into a twin-screw extruder. Inside the heated barrel, rotating screws disperse the colorant through the molten carrier resin. Proper temperature and shear are critical. Excessive heat may damage sensitive pigments. Insufficient mixing can leave streaks or visible specks. The hot strand is cooled, dried, and cut into small pellets. Quality checks usually include color measurement, moisture testing, dispersion inspection, and trial molding. A laboratory result is useful, but production conditions may reveal problems that testing misses.
Tips: Match the carrier resin with the plastic being processed. Keep masterbatch sealed and dry before use. Follow the supplier’s recommended dosage, then adjust through controlled trials. Record melt temperature, screw speed, and cooling conditions. Even experienced operators should check the first molded parts. A small shade difference matters. It may come from pigment concentration, equipment settings, or uneven feeding. Reviewing these details improves repeatability and helps prevent unnecessary material waste.
Colorant masterbatch is a concentrated blend of pigments or dyes, carriers, and additives. It is added during plastic processing to create consistent colour with less handling mess. PlasticsEurope reported global plastics production of 413.8 million tonnes in 2023. This scale makes accurate colour dosing important, especially in packaging, automotive parts, and household products.
Processors usually feed masterbatch with natural resin through a gravimetric or volumetric dosing unit. The pellets melt together in an extruder, injection moulding machine, blow moulding line, or film system. Good carrier compatibility supports smooth dispersion.
Poor compatibility can cause streaks, specks, plate-out, or weak weld lines. A typical starting dosage may range from 1% to 5%, but pigment strength and required opacity determine the final level. MarketsandMarkets estimated the global masterbatch market at over 12 billion US dollars in 2023, showing the sector’s industrial importance. Still, market growth does not guarantee better processing. Trial data matters more.
Tip:
Check melt-flow rate, processing temperature, and let-down ratio before production. Use the same resin grade for colour trials. Keep samples under identical lighting. A perfect colour card may fail beside a finished part. Moisture, screw design, and cooling speed can change the result. My practical concern is simple: operators often adjust dosage before checking dispersion. That choice can increase cost and hide the real process problem. Small trials, documented settings, and regular spectrophotometer checks provide stronger control.
Colorant masterbatch is a concentrated blend of pigments or dyes enclosed in polymer pellets. During extrusion or injection molding, operators mix it with natural resin at a measured let-down ratio. This process provides a repeatable way to create colored products, from food containers to cable jackets. In practice, color matching depends on resin type, temperature, wall thickness, and surface finish. A shade that looks correct on a flat test plaque may appear darker on a ribbed component.
Its main benefit is controlled dosing. Pellets create less airborne pigment dust and help keep production areas cleaner. They also simplify storage because one concentrated material replaces large bags of loose colorant. Good dispersion can improve shade consistency and reduce visible specks, especially when the carrier matches the base polymer. Masterbatch can support faster material changes, too. Less cleaning may reduce wasted resin. It can be cost-effective for steady production.
The benefits have limits. A poor carrier choice may cause weak bonding, surface defects, or unstable processing. Excessive dosing can reduce mechanical performance or alter shrinkage. Some pigments need careful heat and light testing. Color stability cannot be judged from one sample. Small production runs may also leave unwanted inventory. I have seen an acceptable trial fail after cooling because the final part showed gloss variation. That mistake is easy to miss. Reliable use requires documented ratios, test plaques, and production-condition checks. Not every color problem comes from dosing.
Office: (281) 855-2218
Copyright © 2025 Telco Intercontinental Corp. All rights reserved. Privacy Policy | Legal Disclaimer
Telco®, TelcoMotion®, and TelcoGreen® are registered trademarks of Telco Intercontinental Corp.