+1 (281) 855-2218

Which Industrial Vacuum Packaging Machine Is Best in 2026?

Choosing the best Industrial Vacuum Packaging Machine in 2026 is not simply about buying the fastest model. Your product, facility, operators, and packaging materials all influence the decision. A machine that performs perfectly for fresh meat may struggle with delicate bakery products or liquid-rich foods.

Dr. Gordon L. Robertson, a respected food-packaging specialist, has said, “Packaging must protect the product and support the entire distribution system.” That principle remains practical today. A reliable Industrial Vacuum Packaging Machine should create a stable seal, remove air consistently, and maintain performance during long production shifts. Look closely at pump capacity, chamber size, sealing-bar temperature, cycle time, stainless-steel construction, and cleaning access. Small design details matter. A difficult lid or narrow chamber can waste minutes every hour.

Real production experience also exposes weaknesses that brochures often hide. Operators may prefer simple controls over advanced screens. Maintenance teams may value accessible pumps more than impressive speed ratings. Energy use can become significant when the machine runs continuously. Some buyers also underestimate the effect of film thickness, bag size, and product temperature. That mistake can produce weak seals or unnecessary waste.

There is no universal winner. Not yet.

The best choice depends on measurable requirements and honest testing. Request sample trials using your actual products and bags. Check seal strength after cooling, not immediately. Review service response, spare-part availability, and operator training. Even careful evaluations can miss something. That is why a short pilot run often provides more confidence than a polished specification sheet.
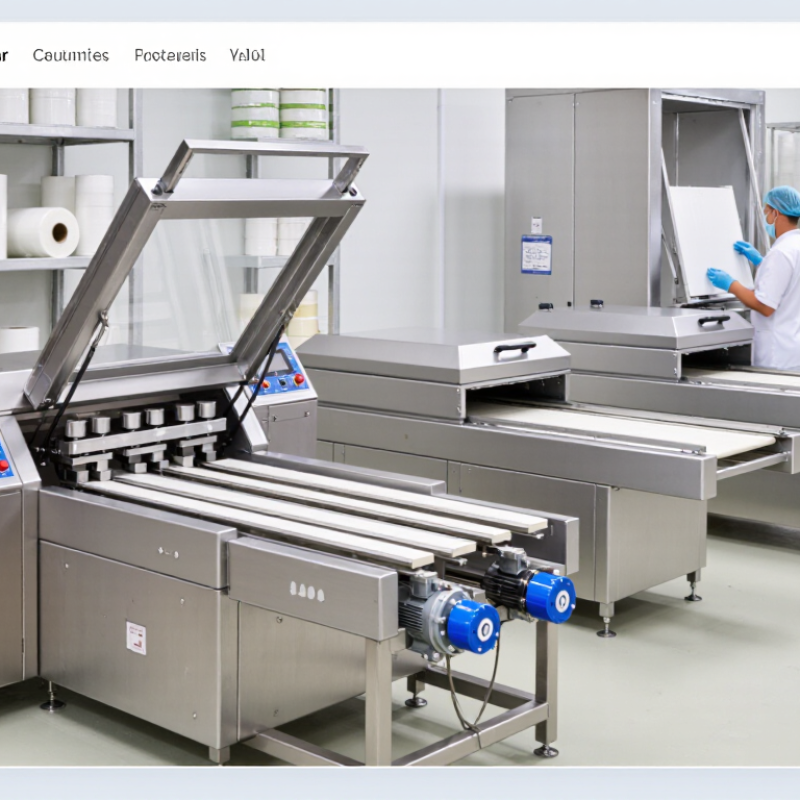
Which Industrial Vacuum Packaging Machine Is Best in 2026?

What Is an Industrial Vacuum Packaging Machine?

An industrial vacuum packaging machine removes air from a package, seals it, and protects products during storage or transport. Unlike small countertop units, it is built for repeated cycles, wider seals, and demanding production schedules. A chamber model places the bag inside an enclosed space, then removes air before sealing. This reduces pressure differences and helps prevent leaks.

The best machine in 2026 depends on the product, package size, and daily workload. A processor handling moist food may need a strong pump, easy cleaning, and adjustable sealing time. A manufacturer packaging sharp components may require thicker bags and controlled vacuum levels. Check seal consistency, chamber dimensions, cycle speed, and maintenance access. A fast machine is not always the best machine. Excessive speed can create weak seals or unnecessary wear. That detail is easy to overlook.

Tips: Test real products before buying. Measure the largest package, observe liquid movement, and inspect seals after cooling. Ask for maintenance records and clear operating instructions. Choose food-contact materials where applicable, and confirm that operators can clean the machine safely. A small trial batch can reveal more than a polished specification sheet. My own evaluation would also include noise, electricity use, and downtime, because these costs are often underestimated. Even experienced teams can miss them.

How Industrial Vacuum Packaging Machines Work

Industrial vacuum packaging machines remove air from a sealed chamber before closing the package. Air leaves the bag. A vacuum pump lowers the chamber pressure, while sensors monitor the cycle. Once the target vacuum level is reached, heated sealing bars press the open edge together. Heat softens the packaging film, and pressure creates a tight seal as it cools.

Many industrial systems also offer gas flushing. After removing oxygen, the machine adds a controlled food-grade gas mixture before sealing. This can protect delicate products from crushing and may slow oxidation. However, gas flushing does not replace proper hygiene, temperature control, or suitable packaging materials. Each product behaves differently. Moist foods, sharp edges, and warm products can affect vacuum performance.

“From hands-on packaging trials, seal quality often matters more than maximum pump speed. A fast pump cannot fix a wrinkled bag or an uneven seal area. Operators should check seal width, residual air, chamber cleanliness, and cycle consistency. Sensors improve repeatability, but they still require calibration and sensible settings. No machine is perfect. Small adjustments may be needed when product size or film thickness changes. For 2026 purchasing decisions, choose equipment with accessible controls, durable sealing components, clear maintenance procedures, and records that support quality checks. Reliability comes from both machine design and disciplined operation.

Key Types of Industrial Vacuum Packaging Machines

Choosing the best industrial vacuum packaging machine in 2026 starts with the product, not the machine price. Different formats solve different production problems.

Single-chamber machines suit small factories, laboratories, and irregular products. Operators place the bag inside, close the lid, and start the cycle. They are flexible but relatively slow.

Double-chamber machines improve throughput because one chamber can unload while the other seals. They fit meat, seafood, cheese, and prepared foods with steady batch sizes.

Rotary belt machines offer faster continuous operation. Their conveyor design handles heavier bags and longer shifts, although cleaning can require more attention.

For high-volume sliced products, thermoform-fill-seal systems form the package from rollstock, vacuum it, and seal it automatically. They reduce manual handling and often improve material consistency.

The choice should reflect measurable production conditions. PMMI’s 2023 U.S. Packaging Machinery State of the Industry identifies food and beverage as a leading machinery demand sector. Meanwhile, the United Nations Environment Programme’s Food Waste Index Report 2024 estimates that 1.05 billion tonnes of food were wasted in 2022. Better sealing cannot solve waste alone, but it can support longer product protection when validated correctly. Chamber depth, pump capacity, seal-bar width, and cleaning access matter more than impressive cycle claims. A factory handling wet products may need stronger vapor protection. A plant using delicate bakery items may need gentler vacuum control.

One detail is often missed. Real output falls during changeovers, sanitation, and film adjustments. I would test the machine with actual products for a full shift. Laboratory results can look perfect. Production rarely does.

How to Compare Performance, Features, and Operating Costs

In 2026, the best industrial vacuum packaging machine is not always the fastest model.

A production test should measure cycle time, vacuum level, seal temperature, and reject rate. I recommend recording results across three shifts, not one impressive afternoon. Dust, moisture, and operator changes expose weak performance. That matters more.

Compare chamber size with your largest regular product, not an occasional oversized item. A reliable machine should offer repeatable vacuum control, adjustable sealing time, clear alarms, and accessible maintenance points.

Use a calibrated gauge when checking vacuum accuracy. Keep records that operators can repeat and managers can review. Check whether sensors detect incomplete seals before packages leave the line.

Tool-free cleaning can save labor, but only if parts are genuinely easy to remove. Do not confuse a long feature list with useful engineering.

Operating cost includes electricity, pump oil, seal wires, bags, downtime, and trained labor. Ask for service intervals and expected consumable life in writing.

A lower purchase price may become expensive after repeated pump repairs. My own early comparisons overvalued rated speed and undervalued changeover time. That was a mistake.

Calculate cost per sealed package using real output, not brochure capacity. Include idle power and cleaning minutes. Then test the machine with your actual products, weights, and moisture levels.

Which Industrial Vacuum Packaging Machine Is Best in 2026?

Which industrial vacuum packaging machine is best in 2026? The practical answer depends on product, throughput, film, and plant conditions. In production trials, the strongest choice is often a machine with stable vacuum control, repeatable sealing, and clear operator feedback. A high-capacity pump matters, but only when it matches chamber size and cycle speed. Excessive pump capacity can increase energy use without improving package quality. Look for stainless construction, tool-free cleaning areas, and seals that remain accessible during inspections. Hygiene is not a marketing detail. It affects downtime and audit confidence.

For wet, irregular, or fragile products, independent control of vacuum, gas flushing, and sealing temperature provides useful flexibility. Sensors should detect incomplete seals, pressure changes, and chamber faults before rejected packs reach distribution. Data logging also helps technicians compare shifts and identify gradual performance drift. Ask for documented test results using your actual product and film. Demonstrations with empty chambers prove very little. A machine may run beautifully for one hour and struggle across a long shift. That limitation deserves attention.

The best 2026 system should fit the whole line, not just the packaging station. Check loading height, conveyor timing, electrical demand, spare-part access, and local service response. Safety guarding must support quick cleaning without encouraging shortcuts. Total cost includes labor, compressed air, electricity, maintenance, training, and unplanned stoppages. No machine is perfect. I would still choose predictable recovery after a fault over a faster advertised cycle. Before purchase, record seal strength, residual oxygen, cycle consistency, and cleaning time across several production days. Let real measurements challenge the sales specification.

SHOP BY BRAND